Steel and aluminum stamping tooling · Automotive industry
Specialized support for stamping dies and sheet metal forming
Diagnosis, maintenance, engineering changes and die tryout, with domestic and international specialists assigned to the needs of each project.
Materials
Steel and aluminum
Service lines
6
Coverage
Mexico and abroad
Specialists
Domestic and international
We support the dies that affect the quality, uptime and stability of your production, with a method documented from start to finish.
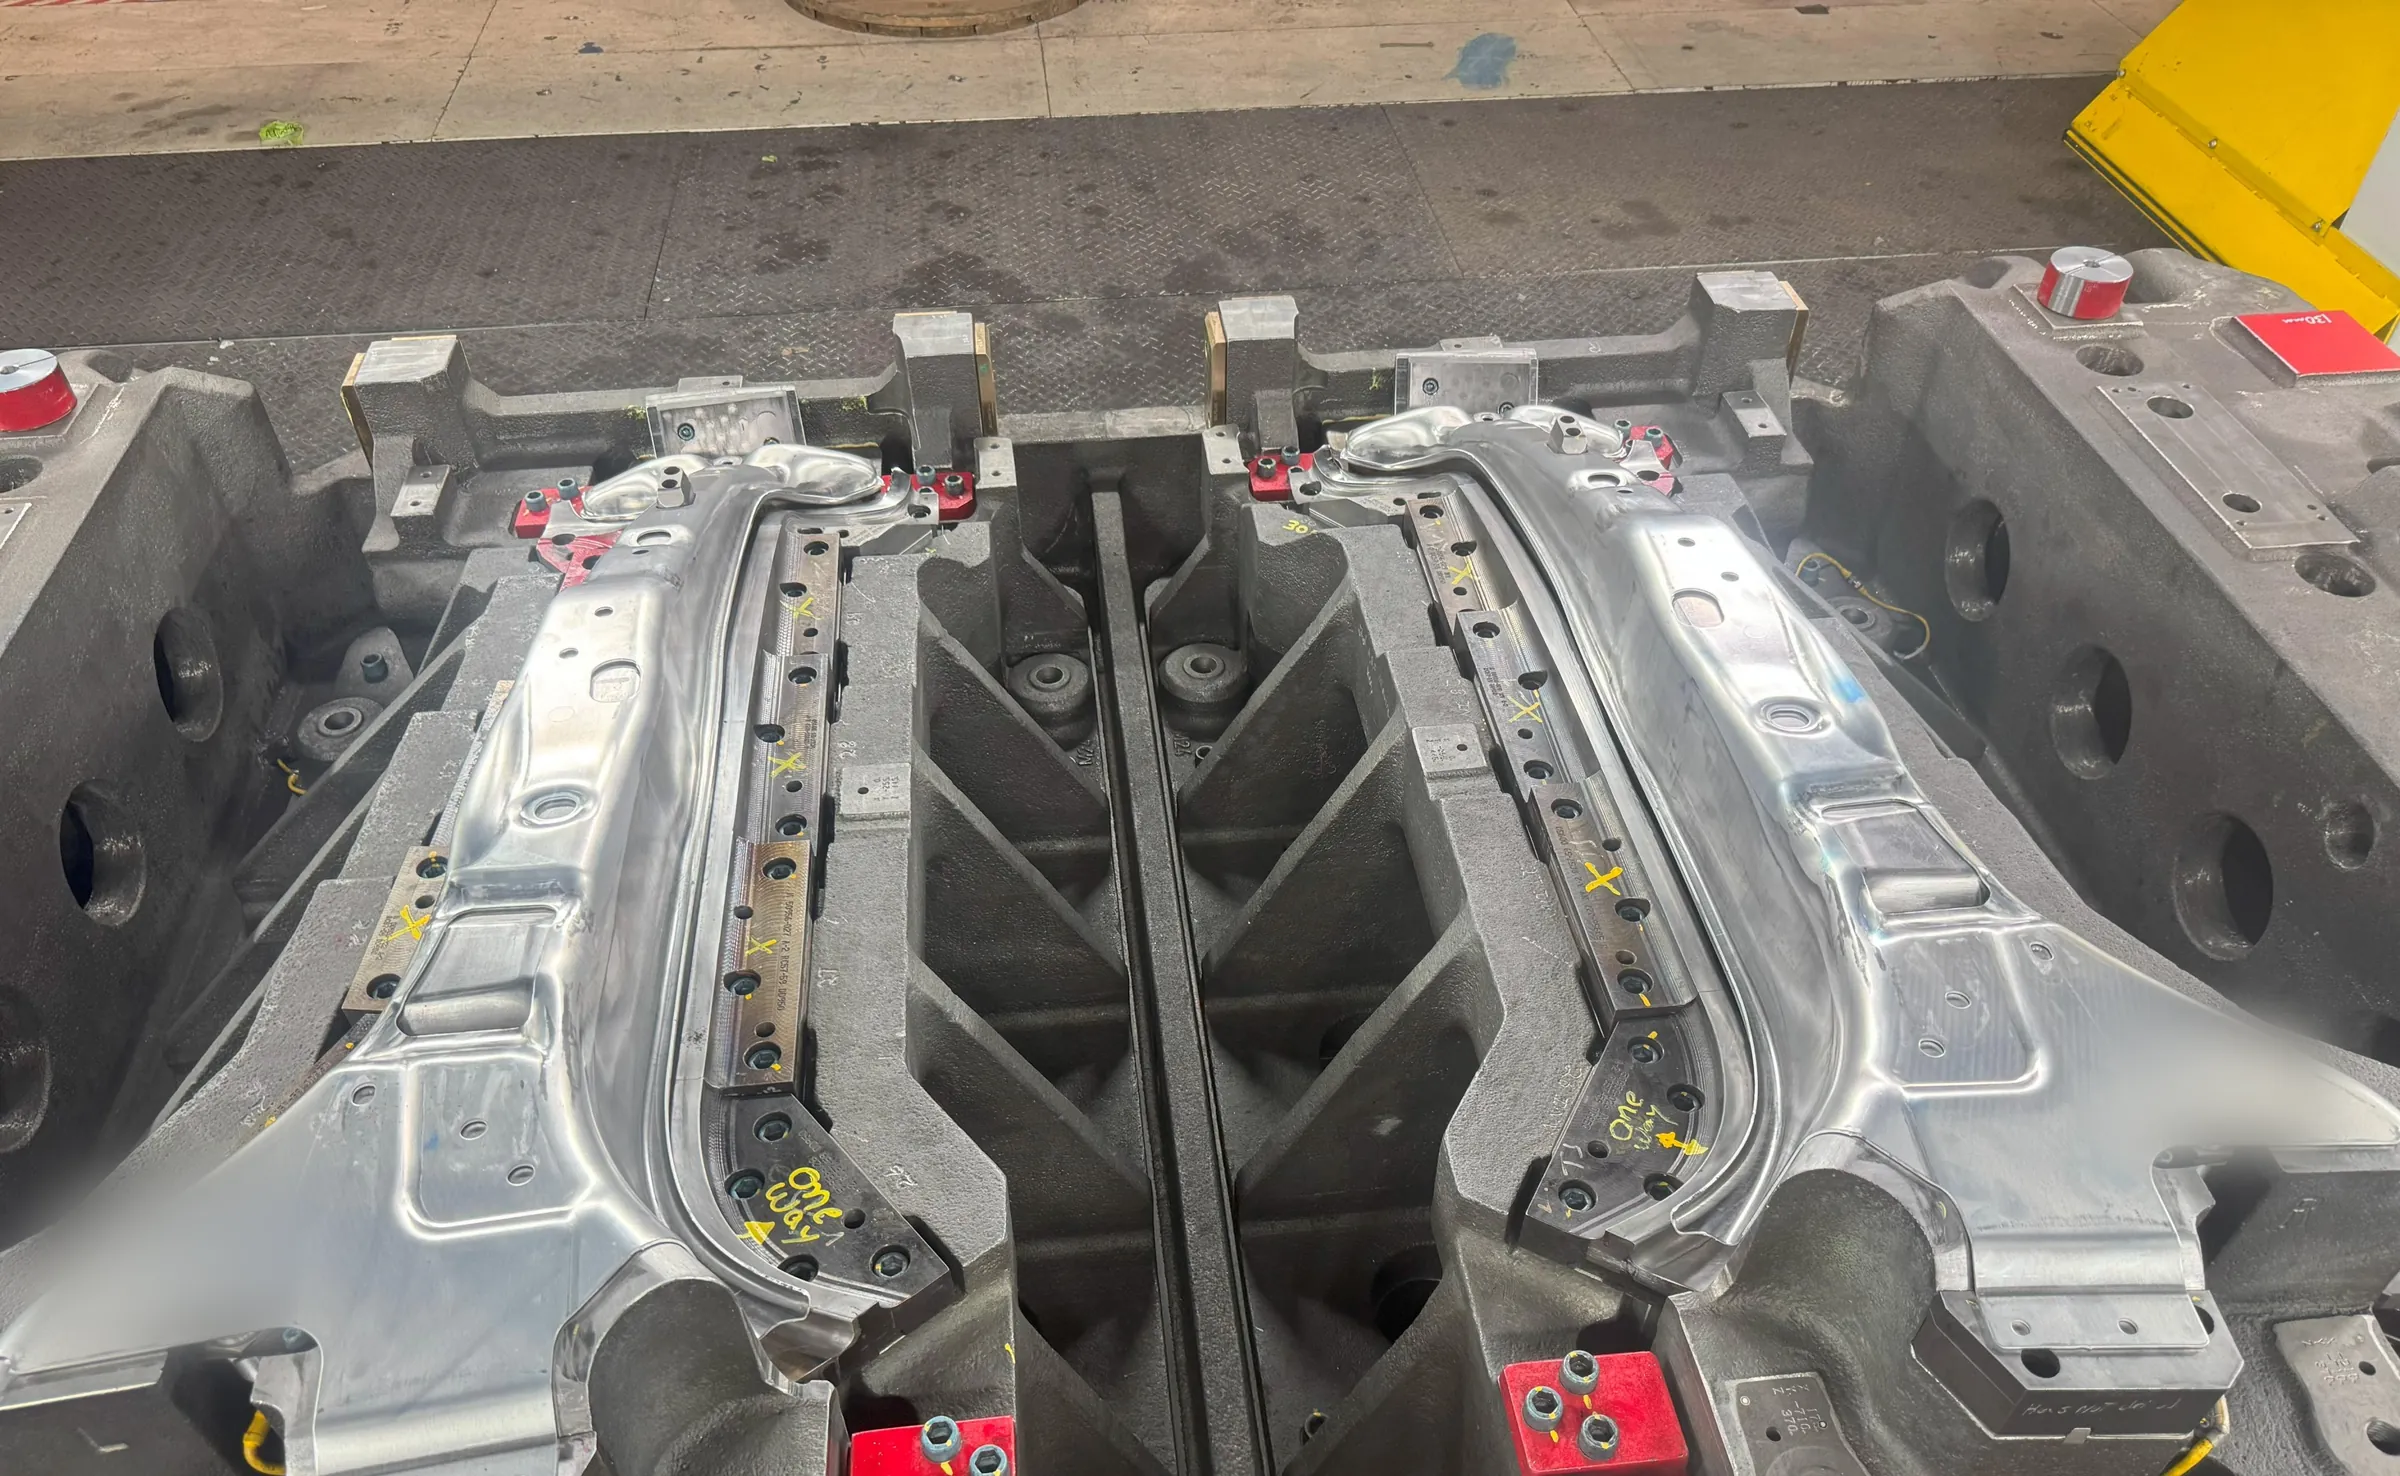
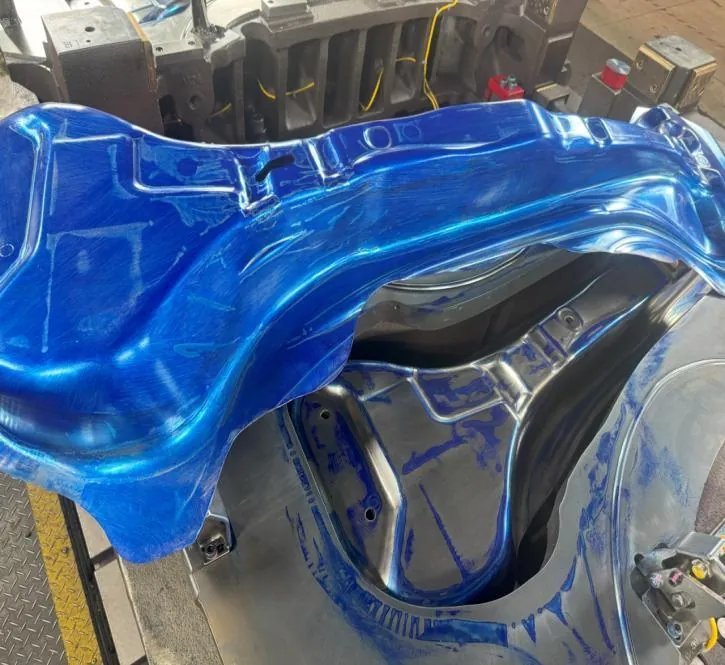
Die under trial with formed panels. Previous team experience.
Services
Six service lines for your tooling
We support dies in production, requested changes and launches, as well as training and project follow-up.
01
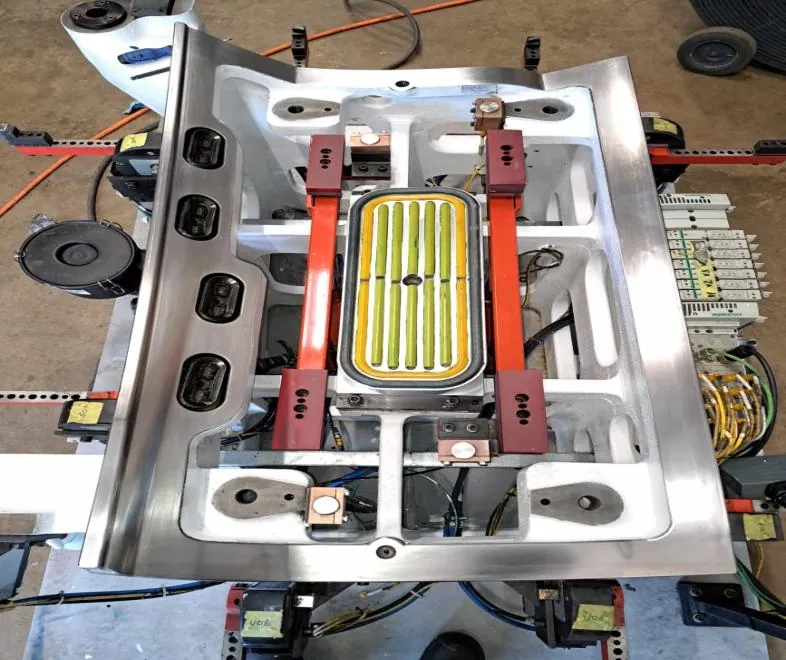
Critical dies
Diagnosis and repair of dies that affect quality, uptime or process stability, including preventive and corrective maintenance.
02
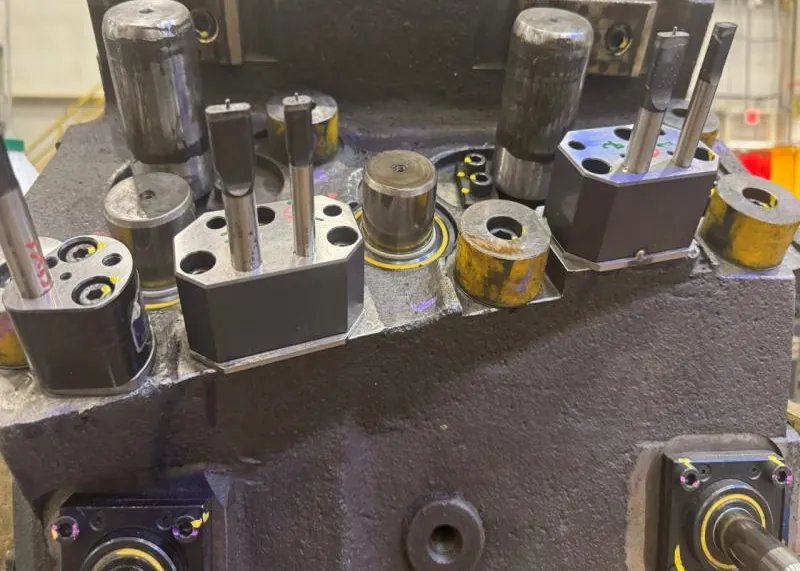
Engineering changes
Evaluation and implementation of requested modifications to holes, trim, flanges or forms, coordinated with engineering.
03
Die tryout and home-line support
Static and dynamic review, press or line trials and adjustment for launches and panel approval.
05
SPM increase
Analysis of the constraints that limit strokes per minute, considering method, labor, machine and material.
06
Project management
Activity planning, specialist coordination and tracking of progress and open items with your team.
01 Critical dies
02 Engineering changes
03 Die tryout and home-line support
04
04 Training
05
05 SPM increase
06
06 Project management
How we work
From assessment to follow-up
01
Assessment
We review the die condition and the available quality information.
Assess
02
Intervention proposal
We define the activities, resources and press time required.
Plan
03
Coordinated execution
We carry out the work with the specialized staff the project requires, in coordination with your plant.
Execute
04
Verification and follow-up
We document results, open items and control points.
Verify
Specialized staff
Domestic and international specialists
We bring in domestic or international specialized labor according to the requirements and availability of each project.
Each request is reviewed to define the right staff and logistics.
Countries where we can work
 Mexico
 Brazil
 United States
 Argentina
And other countries, depending on the project.
Team experience
Documented interventions
A selection of the team's previous experience. Each one states what was done, what was verified and what remained open.
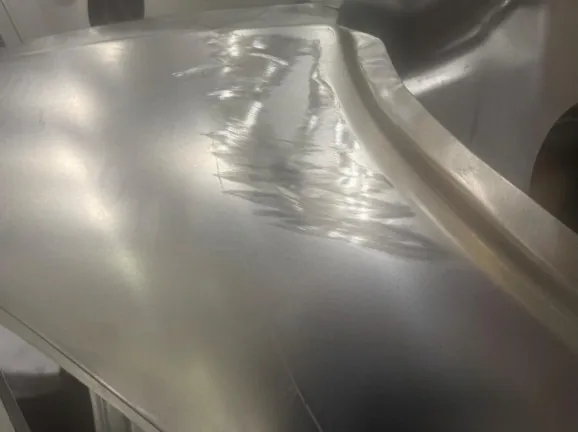
Defect
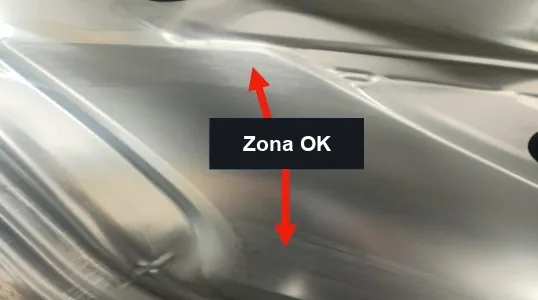
With tape
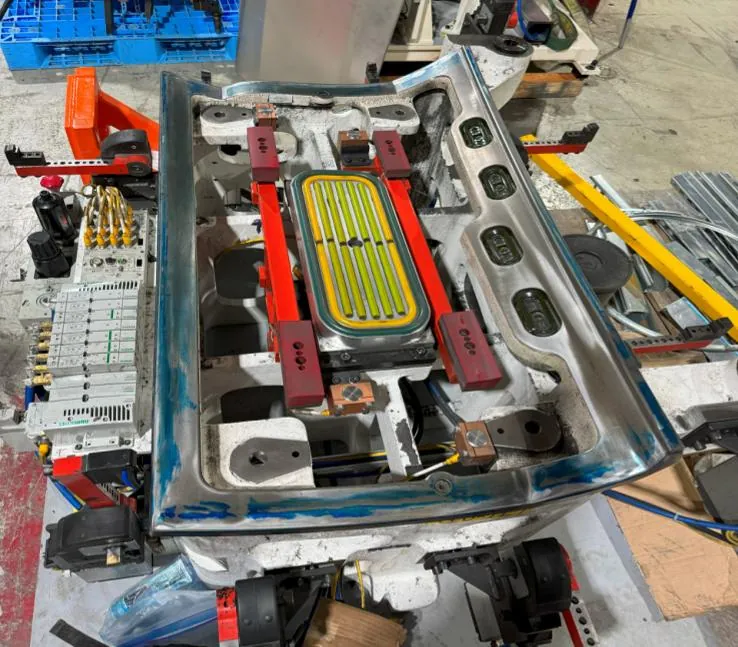
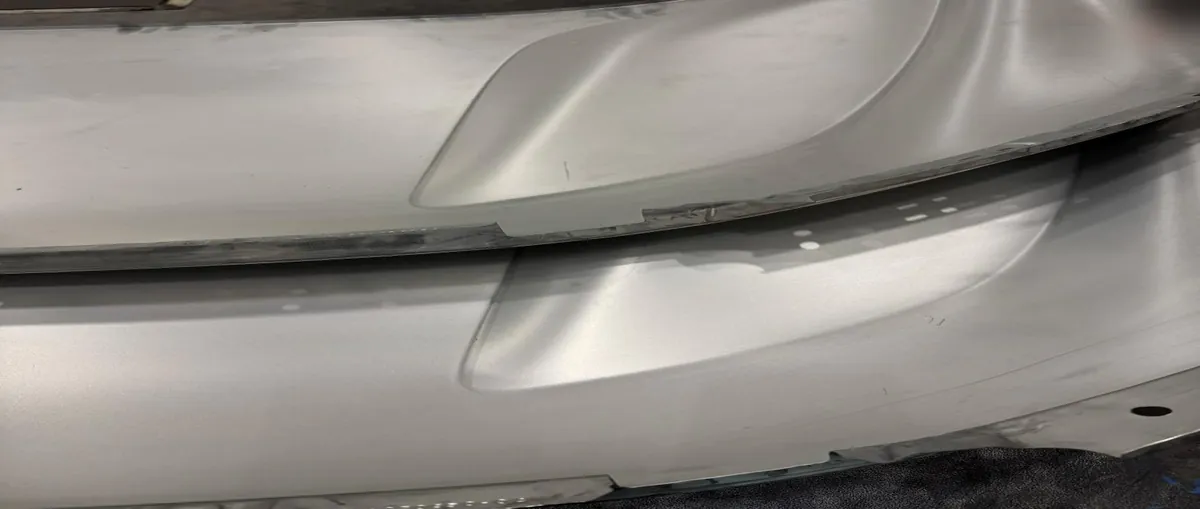
Draw die, OP10 · Aluminum
Quality defects in operation 10
OP10 is the most critical operation to adjust. A test placing tape on the bead radius to correct the panel defects.
- With the tape, the checked area is OK
- Welding on the bead radius
Before
After
Roll hemming tool
Tool maintenance and recovery
Blue contact inspection, recovery of worn and deformed areas, and adjustment using the panel as a reference.
- Before and after comparison documented
- Production validation not included in the report
Panel dies, OP10 to OP40
Correction of die setup conditions
Clearance and steel angle adjustment, redesign of damaged detectors, and guide and sensor adjustment across several operations.
- OP40 trial with no scratches or hard marks in the treated area
- Activities rescheduled in other operations
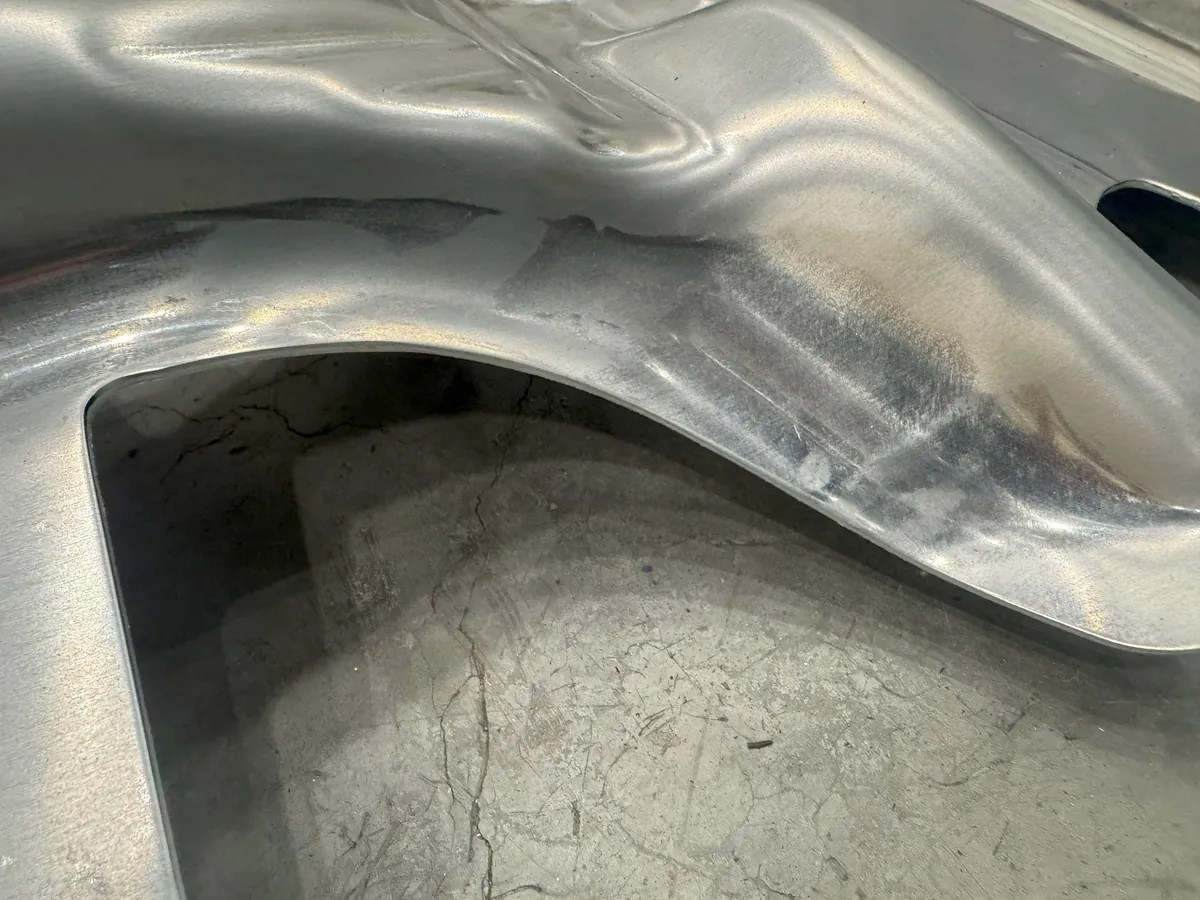
Structural reinforcement die, OP10 to OP40
Die tryout and buy-off support
Calibration, contact review, weld repair of deformed areas and adjustment in the press.
- Trial with no trim distortion and OK condition at OP40
- Production follow-up and a positioning adjustment pending
Tell us what is happening with your die
Describe the process, the operation and the issue you are seeing. We will review your request and reply to arrange a technical conversation or a quote.