Team experience
Documented interventions
Previous projects of our team. For each one we state what was done, what was verified and what remained open. Customer names, brands and engineering numbers are omitted.
Before
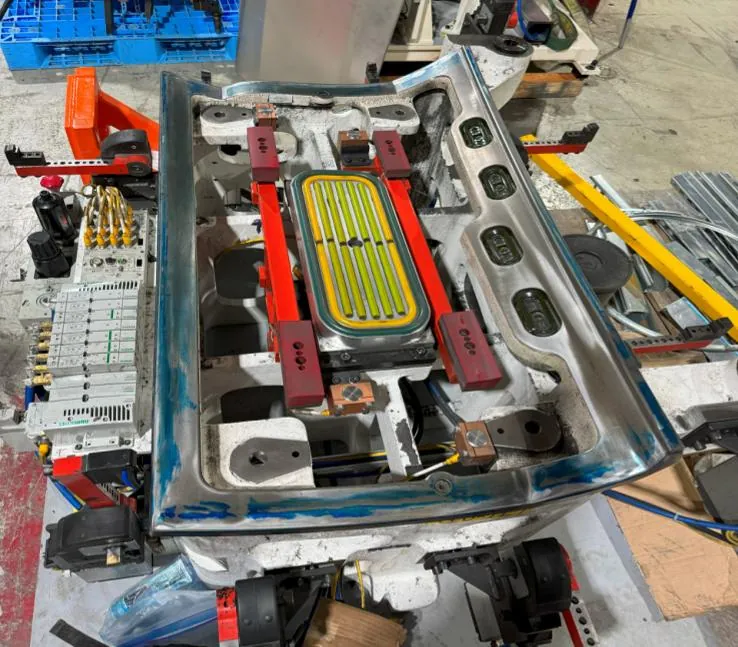
After
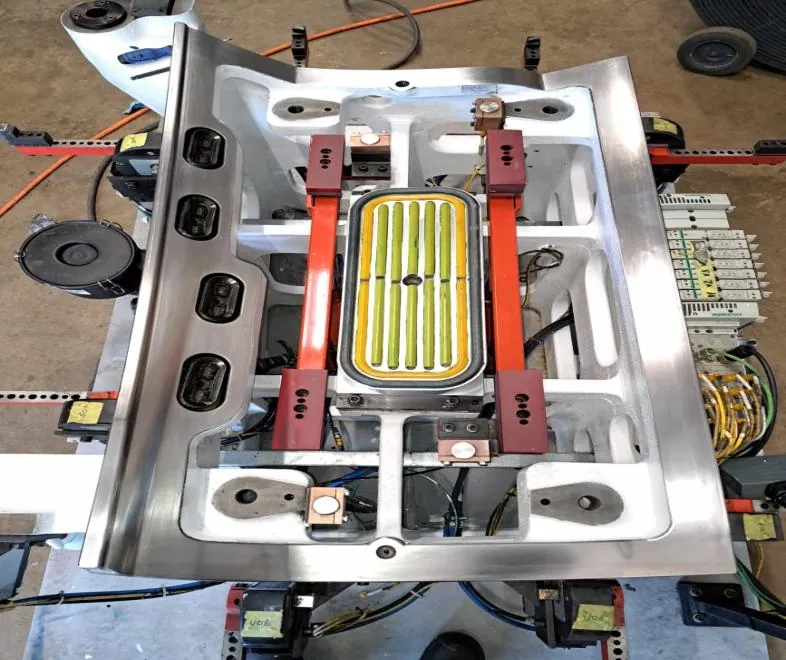
Roll hemming tool
Maintenance and recovery of roll hemming tools
Need
Wear and deformation on the working surface and trim areas, detected through a blue contact inspection.
Intervention
Welding on the surface and trim, heating of deformed areas and adjustment with abrasive tools, using the panel as a reference.
Documented verification
Visual comparison of the tool before and after the work.
- Status: Work completed; result observed in the shop.
- Follow-up: The report does not include later validation in production.
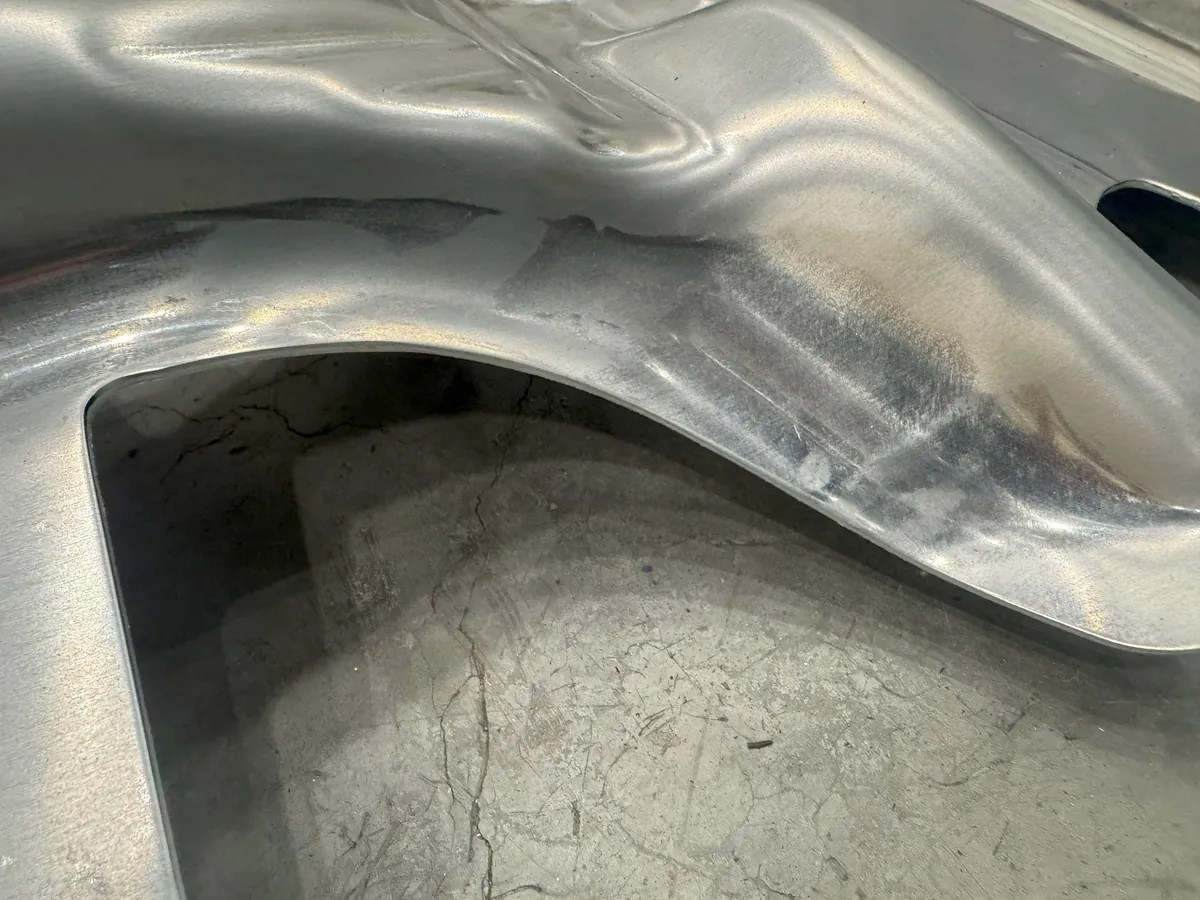
Wrinkles
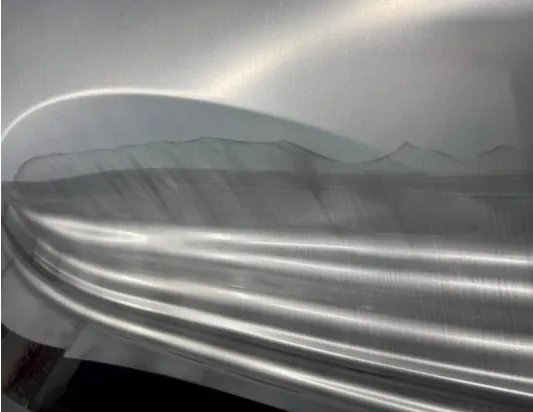
Split
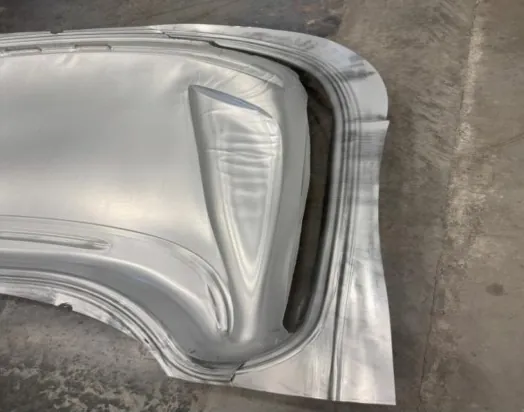
Intervention
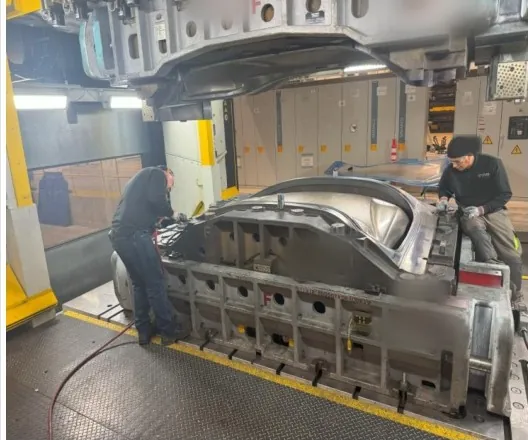
Draw die, OP10 · Aluminum
Wrinkles and split on an outer hood
Need
Wrinkles and a split on the drawn panel. OP10 is the most critical operation to adjust.
Intervention
Blank holder contact adjustment in the tryout press, checked with blue contact marks.
Documented verification
The photos show the defect and the intervention; the result is not documented in them.
- Status: Work completed.
- Follow-up: Document the result of the press trial.
Defect
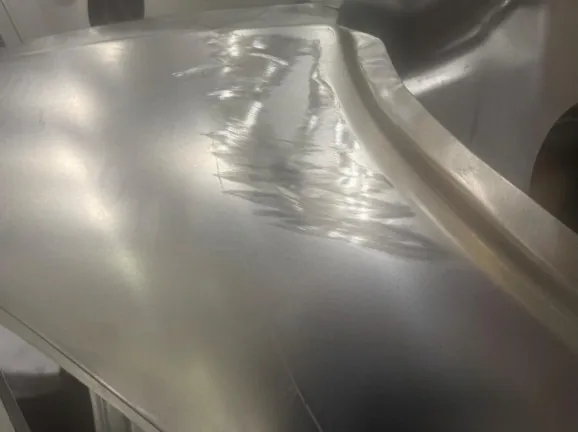
Tape test
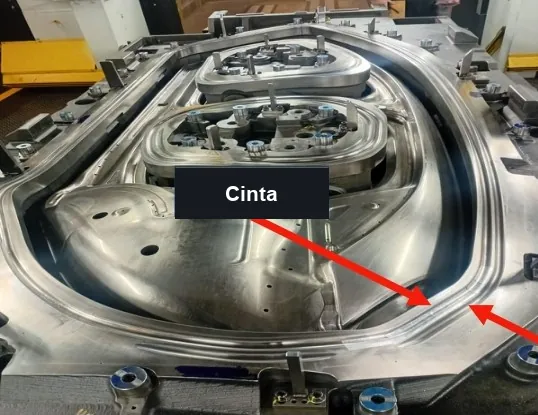
With tape
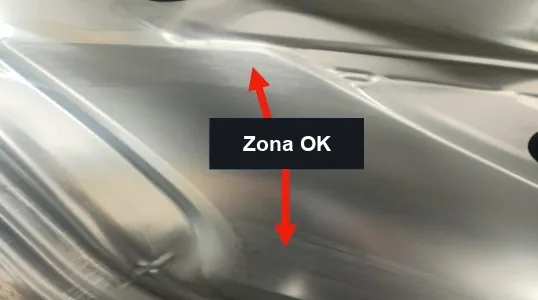
Draw die, OP10 · Aluminum
Quality defects and tape test on the beads
Need
Quality defects on the surface and on the radius of the drawn panel.
Intervention
A test placing tape on the radius of the die beads.
Documented verification
With the tape, the checked area of the panel is OK.
- Status: Result observed in trial.
- Follow-up: Welding on the bead radius.
OP40 trial
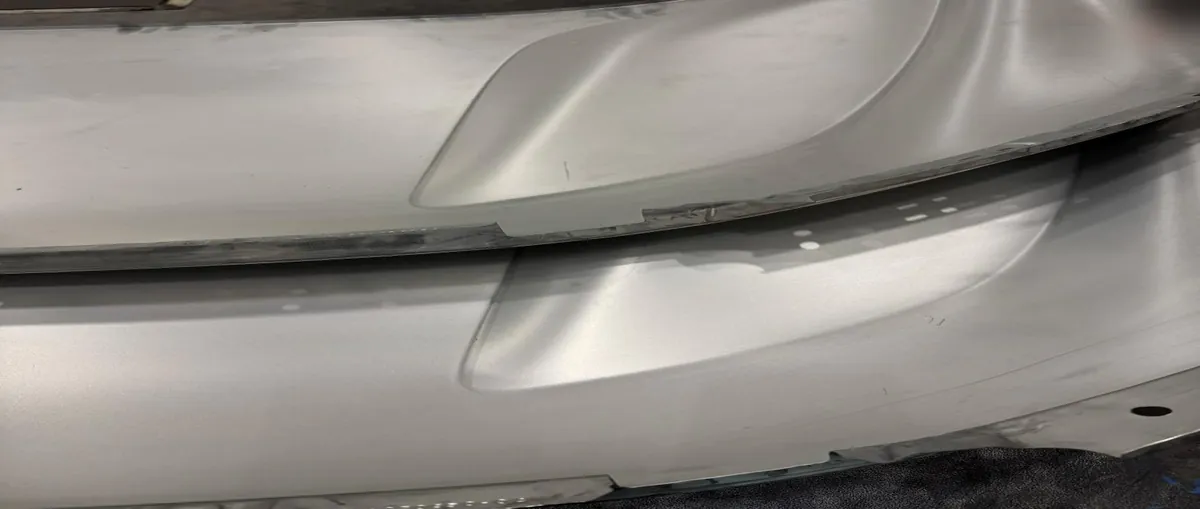
Automotive panel dies, OP10 to OP40
Correction of setup conditions across several operations
Need
Splits in forming, hard marks and scratches on the panel, buttons out of position after earlier modifications, tight clearances and steel angles causing excessive contact.
Intervention
Polishing and machining to add clearance, redesign and manufacture of damaged detectors, guide and sensor adjustment, weld rebuild and button adjustment, angle change on upper steels and clearance adjustment.
Documented verification
Sensor function confirmed in the tryout press (OP10). Press trial at OP40: no scratches or hard marks in the treated area.
- Status: Partial result.
- Follow-up: Clearance and scrap issues at OP20, guide angle at OP30 and dowel pins at OP40 were rescheduled.
In the press
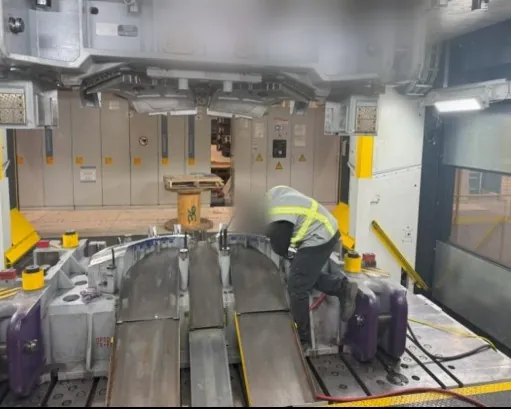
No distortion
Automotive structural reinforcement die, OP10 to OP40
Tryout and buy-off support
Need
Binder contact below the program standard, balancers without contact, scratches on the upper die, split and deformation at trim.
Intervention
Guide adjustment for blank location, balancer calibration, radii on guides, temporary tape on the line, weld rebuild and adjustment in the press. Preventive maintenance at OP40 including correction of weld porosity.
Documented verification
Trial with no trim distortion (OP20). OK condition when the previous repairs were confirmed in the press (OP40).
- Status: Result observed in trial.
- Follow-up: Follow-up in the next production run. Alignment of steels lacking dowels or keys still pending.
Previous team experience. Customer names, brands and engineering numbers are omitted; techniques, measurements and parameters are shared only with the corresponding customer.
Tell us what is happening with your die
Describe the process, the operation and the issue you are seeing. We will review your request and reply to arrange a technical conversation or a quote.