Services
Services for stamping tooling
Six service lines for steel and aluminum dies, mainly for the automotive industry. Each intervention is defined from an assessment of the die and your plant's objectives.
01
Critical dies
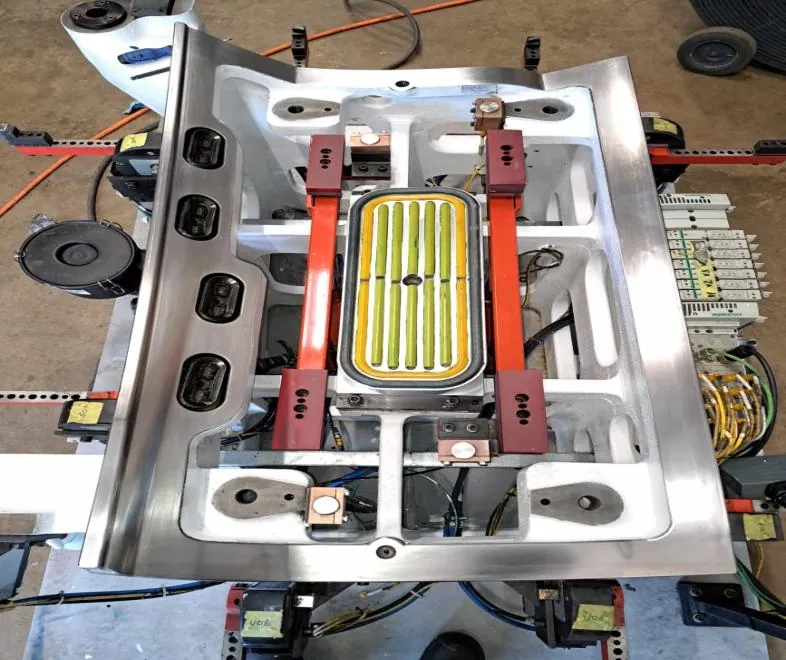
A critical die is one that directly affects the time, cost and quality indicators of your production.
What we address
Panel defects such as splits, wrinkles, dents (low spots and high spots), double lines and burrs, as well as surface wear, clearances and components that compromise process stability.
Defects we address
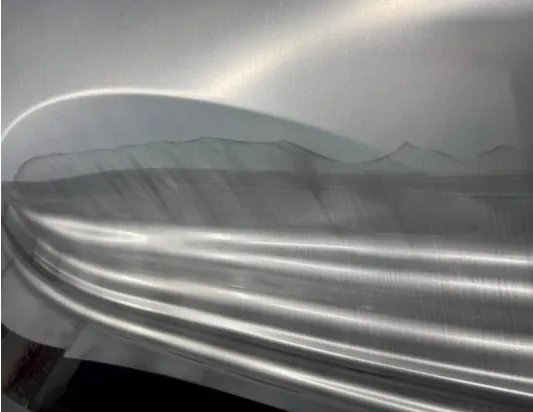
Wrinkles
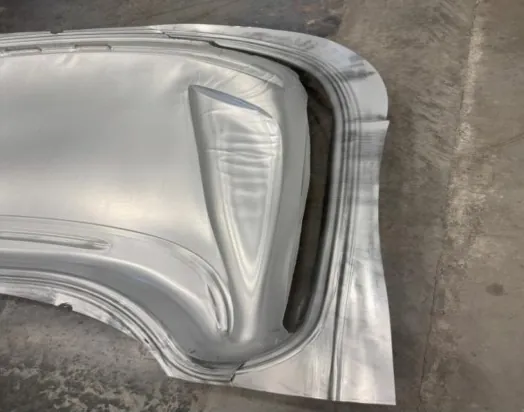
Split
Burrs
Panels from the team's previous work.
General scope
- Assessment of the current die condition against tooling standards.
- Action plan with the time, resources and press time required.
- Preventive and corrective maintenance, surface recovery and die spotting.
- Panel approval method defined with your team, for example CMM report, checking fixture or assembly.
- Line follow-up and definition of control points.
How we work with you
We start from the available quality information and, when it exists, the last panel produced as a reference. Activities are coordinated with your tooling, quality and production teams.
02
Engineering changes
Modifications to the original design requested by the customer or by the next process.
What we address
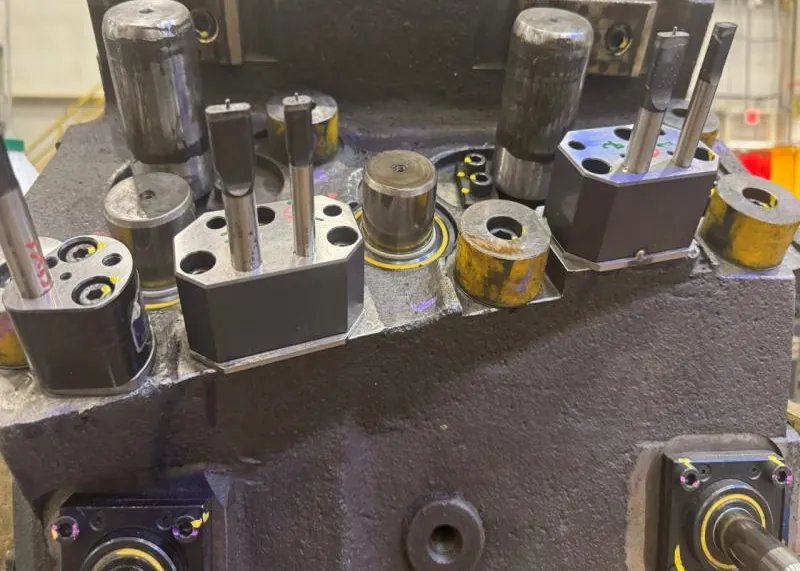
Changes to round and slotted holes, trim lines, flanges or forms that must be transferred to the die without compromising other panel features.
General scope
- Evaluation of the requested change and its effect on other panel features.
- Trials and a reference panel to assess the proposal before modifying the die.
- Intervention alternatives agreed between engineering and tooling.
- Change documentation with the measurements needed for validation.
How we work with you
Every change is validated with your engineering team before and after the work. Techniques and parameters are defined for each case rather than applied as a general recipe.
03
Die tryout and home-line support
Launch support for new programs, from die review to panel approval.
What we address
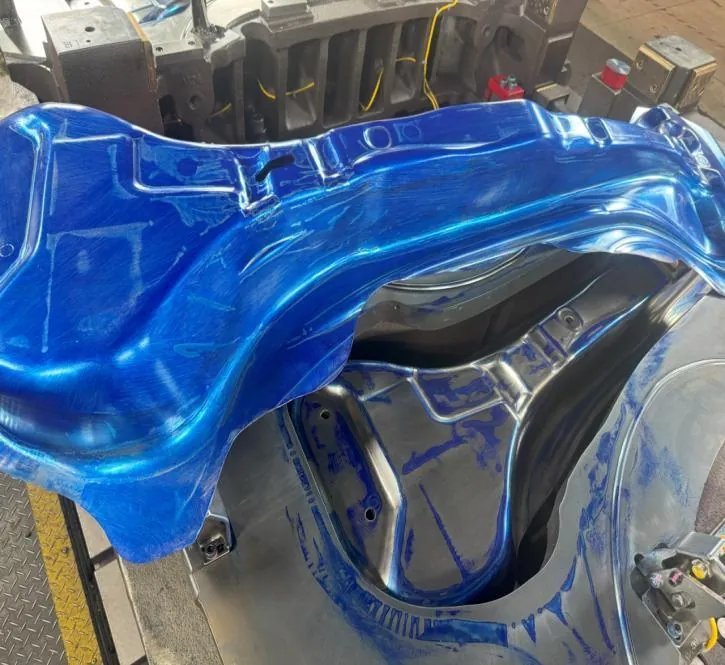
New or modified dies that must reach the required quality and function in the press. Tryout covers die trials and adjustment in a press; home-line support covers trials and adjustment on the customer's production line.
General scope
- Static review: component function against the customer's checklist.
- Dynamic review on the line: panel quality, scrap flow, lifters, cams and other functions.
- Calibration, die spotting and correction of quality defects to the required level.
- Support through panel approval and follow-up during the first production runs.
How we work with you
We work in the press or on the line defined by the program, in coordination with your launch, quality and production teams.
04
Training
Knowledge and skills for die maintenance, with basic and advanced techniques.
What we address
Tooling teams that need to strengthen or standardize their maintenance and spotting skills.
General scope
- Theoretical and practical assessment of the current skill level.
- Training plan on demand or scheduled, short or long term.
- Training with manuals and hands-on hours.
- Follow-up on skill progress.
How we work with you
Content and duration are agreed with your company based on the initial skill level of the staff and the plant's objectives.
05
SPM increase
SPM stands for strokes per minute. We analyze what limits the rate of your process.
What we address
Stamping processes whose rate is limited by die, machine, material or work method conditions.
General scope
- Process analysis and identification of machine, labor, material and method constraints.
- Action plan with the departments involved, organized as a work cell.
- Production parameters defined so that machinery and equipment are not put at risk.
- Follow-up on completion of the agreed activities.
How we work with you
Rate targets are set with your team based on the analysis, without compromising panel quality or equipment safety.
06
Project management
Coordination of technical activities so that each project moves forward with visible owners, dates and open items.
What we address
Tooling projects that involve several operations, specialists or plant areas and need structured follow-up.
General scope
- Activity and resource planning.
- Coordination of the specialized staff the project requires.
- Tracking of progress, results and open items.
- Progress reports for your team.
How we work with you
The reporting format and follow-up frequency are agreed at the start of each project.
Specialized staff in every service
Across all services we bring in domestic or international specialized labor, according to the requirements and availability of each project.
Confidential technical information
Procedures, measurements and parameters of each intervention are shared only with the corresponding customer. This page describes our services in general terms.
Which service does your project need?
If you are not sure, describe the issue you are seeing and we will help you define the right assessment.